Discover Exciting Plastic Manufacturing Jobs at Allied Plastics

How to Choose a Steel Pipe Making Machine?

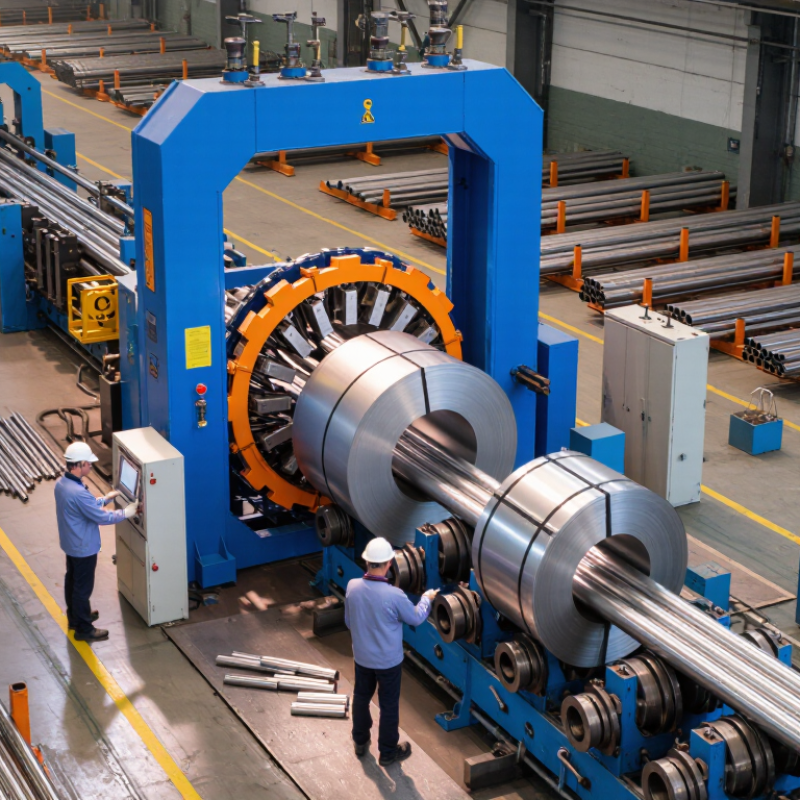
Choosing a Steel Pipe Making Machine is not simply a question of production speed. The right line must match your pipe dimensions, steel grades, expected output, and available floor space. A machine built for thin-wall tubing may not suit heavy-wall pipe, even when both products look similar in a catalog. Define your product range clearly: outer diameter, wall thickness, pipe length, and required tolerances. Be specific.

The forming method, welding process, and sizing system affect both product quality and operating costs. Check whether the machine can handle your planned material thickness and whether changing rolls between sizes is practical. Ask about line speed under real production conditions, not only the maximum listed in a brochure. Details matter. Review the controls, cutting equipment, safety features, power needs, and maintenance access. A crowded layout can make routine servicing harder than expected. Ask the supplier for references, sample pipes, technical drawings, and a factory acceptance test plan. Confirm what installation, operator training, spare parts, and after-sales support include. Compare total ownership costs, including tooling, energy, and downtime, rather than purchase price alone. No machine is perfect. Some specifications may need compromise, and that deserves honest discussion before ordering. A careful comparison helps you choose equipment that fits actual production needs, instead of paying for capacity or features your operation may not use.
How to Choose a Steel Pipe Making Machine?

Define Pipe Requirements: ASTM A53 Covers NPS 1/8–26

Before choosing a steel pipe making machine, define the required size range, wall thickness, grade, and production method. ASTM A53/A53M covers pipe from NPS 1/8 through NPS 26, but NPS is a nominal designation, not the measured outside diameter. ASME B36.10M lists an outside diameter of 0.405 inches for NPS 1/8 and 26 inches for NPS 26. That is a substantial forming range. Not a small adjustment.

These dimensions affect forming rolls, sizing stands, tooling changes, and line layout. For example, a machine set up for small-diameter pipe may not accommodate the tooling or forming loads required for larger pipe. Wall thickness matters too: confirm the schedules and tolerances needed for your orders against the relevant ASTM requirements. Standards define the product; they do not guarantee that one mill configuration can efficiently produce every size.

Ask suppliers for a documented size-and-thickness matrix, then compare it with your target products and ASTM A53 pipe type. Check changeover time and trial-run records, not just maximum capacity. Measure twice. I would also leave room for uncertainty: published capacity figures can depend on material grade, wall thickness, and operating speed. Verify those assumptions using the same product specification you plan to manufacture.

Compare ERW, Spiral, and Seamless Processes for Your Target Diameter

How to Choose a Steel Pipe Making Machine?

Start with the finished pipe’s outside diameter, wall thickness, grade, and annual volume—not a machine brochure’s maximum figure. ERW forms strip into a tube and welds one longitudinal seam. It often suits small-to-medium diameters and high-volume orders. Its workable range depends on strip width, forming stands, and welder capacity. Check the actual mill limits.

Spiral welding uses coiled strip and can produce large-diameter pipe without requiring equally wide plate. It may suit water, piling, or transmission projects, but seam length and inspection requirements affect output. Seamless production pierces and rolls a solid billet. No weld seam. It can fit demanding pressure applications, though investment and energy needs are often higher. World Steel Association’s World Steel in Figures 2024 reports 1,892.2 million tonnes of crude steel production in 2023. That is useful supply-chain context, not a pipe-machine sizing rule.

Tips: Ask suppliers to demonstrate your target diameter, wall thickness, and grade on the proposed line. Compare changeover time, scrap rate, and measured tolerances. A maximum diameter alone can mislead. I would also verify coil or billet availability before choosing; that step is easy to overlook.

How to Choose a Steel Pipe Making Machine? - Compare ERW, Spiral, and Seamless Processes for Your Target Diameter
The diameter ranges below are indicative industry ranges, not fixed limits. Actual capacity depends on mill design, steel grade, wall thickness, product standard, and production configuration.
Comparison dimension ERW pipe mill Spiral welded pipe mill Seamless pipe mill
How the pipe is made Steel strip or coil is roll-formed into a tube. The edges are joined by high-frequency electric resistance welding, usually along a longitudinal seam. Coil strip is formed helically into a cylinder and joined with a spiral seam, commonly using submerged arc welding (SAW). A solid billet is heated, pierced, and rolled or drawn into a hollow tube. The finished pipe has no welded seam.
Indicative outside-diameter range Often about 20–610 mm, depending on the mill. Many production lines focus on smaller and medium diameters. Often about 400–3,000 mm; specialized line designs may cover different ranges. Commonly about 13.7–660 mm across established production routes; the available range varies substantially by process and equipment.
Best fit by target diameter A strong option for small-to-medium diameters when the required size fits a dedicated high-speed line. Well suited to large-diameter pipe, especially when diameter flexibility and long pipe sections are important. Choose when the specification requires seamless construction or when the target product range and quality requirements justify billet-based production.
Typical wall-thickness considerations Commonly used for thin- to medium-wall products; feasible thickness depends on diameter, steel grade, welding system, and line configuration. Can produce substantial wall thicknesses for large-diameter pipe, subject to forming and welding capacity and the required pipe standard. Can cover a range of wall thicknesses, but achievable combinations of diameter and thickness depend on the chosen piercing and rolling route.
Seam and inspection Has one longitudinal weld seam. Production typically includes weld monitoring and specified nondestructive examination and testing. Has a helical weld seam. Weld quality, inspection method, and acceptance criteria are set by the applicable product specification. Has no weld seam, but still requires inspection and testing for dimensions, surface condition, and material properties.
Production and input material Uses coil or strip and is well suited to continuous, high-volume production of a defined size range. Uses coil strip; changing forming settings can allow a line to cover multiple diameters within its designed operating range. Uses billets rather than coil. The hot-working process and multiple production stages generally require more energy and process control.
Typical application areas Structural tubing, water and gas lines, mechanical tubes, and other products permitted by the applicable specification. Large-diameter water transmission, piling, structural applications, and certain oil and gas pipeline products where the specification allows spiral-welded pipe. Applications requiring seamless pipe, including selected high-pressure, mechanical, boiler, and energy-sector uses, subject to grade and standard.
Main trade-off Efficient for its designed size range, but a major diameter change may require different tooling or another line. Offers large-diameter capability and size flexibility, but spiral-weld requirements must be acceptable for the intended service and specification. Avoids a weld seam, but billet processing typically involves higher equipment investment and production cost than welded routes.
Practical selection rule Select ERW when the target diameter, wall thickness, grade, and product standard fit a high-volume longitudinal-weld line. Select spiral welding when large diameters are central to the product mix and the required standard permits the helical seam. Select seamless production when the purchase specification explicitly requires seamless pipe and the expected demand supports billet-based manufacturing.

Match Mill Capacity to Pipe OD, Wall Thickness, and Steel Grade

Choose a pipe mill around its working envelope, not its advertised maximum diameter. Define the smallest and largest outside diameters, wall thickness range, steel grades, coil width, and target speed. A mill rated for 12-inch pipe may not sustain thick-wall, high-strength production at nameplate speed. Ask for a capacity matrix covering diameter, thickness, grade, and speed. It should also state forming and welding limits. Not enough. Confirm performance with production coils, not just a sample calculation.

Steel grade and dimensions change the load. API Specification 5L includes X52 and X70 grades, with minimum yield strengths of 52,000 and 70,000 psi. Higher strength can increase forming demands, though actual loads depend on chemistry, thickness, and mill design. ASTM A53 lists an 8.625-inch outside diameter for NPS 8 pipe; wall thickness varies by schedule. That difference matters to roll setup and weld control. The World Steel Association’s World Steel in Figures 2024 reports 1,892.2 million tonnes of crude steel production in 2023. This signals the scale of steel supply, but it does not determine mill size. A neat specification sheet can still mislead; leave room for trial runs and changeovers.

Evaluate Forming, Welding, Sizing, and Cutting Stations

How to Choose a Steel Pipe Making Machine?

The forming station sets the pipe’s shape and influences how smoothly the strip reaches the weld. Check the forming range, roll adjustment, and changeover time for your planned diameters and wall thicknesses. Look for stable strip guidance; a wandering edge can create trouble later. Small details matter.

At the welding station, assess whether the process can maintain a consistent seam at your target speed. Ask how operators monitor heat input and weld quality, and inspect sample welds if possible. A polished specification sheet is not enough. Production conditions are messier. Consider access for routine checks and how quickly an operator can respond to a seam issue.

Sizing rolls should correct the pipe’s final diameter and roundness without excessive adjustment. Review the available sizing range and how settings are documented between jobs. At the cutting station, check length accuracy, cut-face quality, and how the system tracks moving pipe. Poor synchronization can leave uneven ends or create avoidable scrap. Compare the complete line under realistic material and speed conditions, not just each station in isolation. A fast line may still disappoint if frequent size changes require lengthy setup. That trade-off deserves a close look.

How to Choose a Steel Pipe Making Machine?

Evaluate the forming, welding, sizing, and cutting stations using the practical selection checks shown below.

Counts represent the number of selection checks listed for each station, not machine performance ratings. Consider material and pipe specifications when comparing equipment.

Verify Inspection Needs Against API 5L PSL 1 and PSL 2 Criteria

A steel pipe line should be selected against the ordered API 5L requirements, not a generic “PSL 2-ready” claim. API Specification 5L, 46th edition, sets different requirements for PSL 1 and PSL 2 covering chemistry, mechanical testing, toughness, and inspection. Exact obligations vary by grade, dimensions, and delivery condition. For example, API 5L specifies minimum yield strengths of 360 MPa for X52 and 485 MPa for X70. These figures guide material and process checks, but they do not define every acceptance test. Small details matter.

Check that the line can perform the required weld-seam nondestructive examination, hydrostatic testing, dimensional checks, and sample testing. Confirm coverage, calibration, and record retention before comparing production speed. The World Steel Association’s World Steel in Figures 2024 reports 1,892.2 million tonnes of global crude steel production in 2023; that broad scale makes consistent material traceability important, though it is not a pipe-specific measure. A practical weakness in some machine evaluations is treating PSL 2 as one fixed inspection package. It is not. Ask for a requirement-by-requirement matrix tied to the actual pipe order, then verify it against the applicable API 5L edition and customer specification.